


Why Outdoor LED Housings Need Wet-Adhesion Thinking (Not Only Cross-Cut)
Outdoor Linear Lighting Solutions for Architecture and Infrastructure
The failure that dry tests miss
On outdoor façades and bridges, coatings often pass a dry cross-cut check, then blister or lift after salt fog, condensation, or long wet service. If the submittal only scores the dry test, a housing finish can still fail once moisture reaches the metal interface.
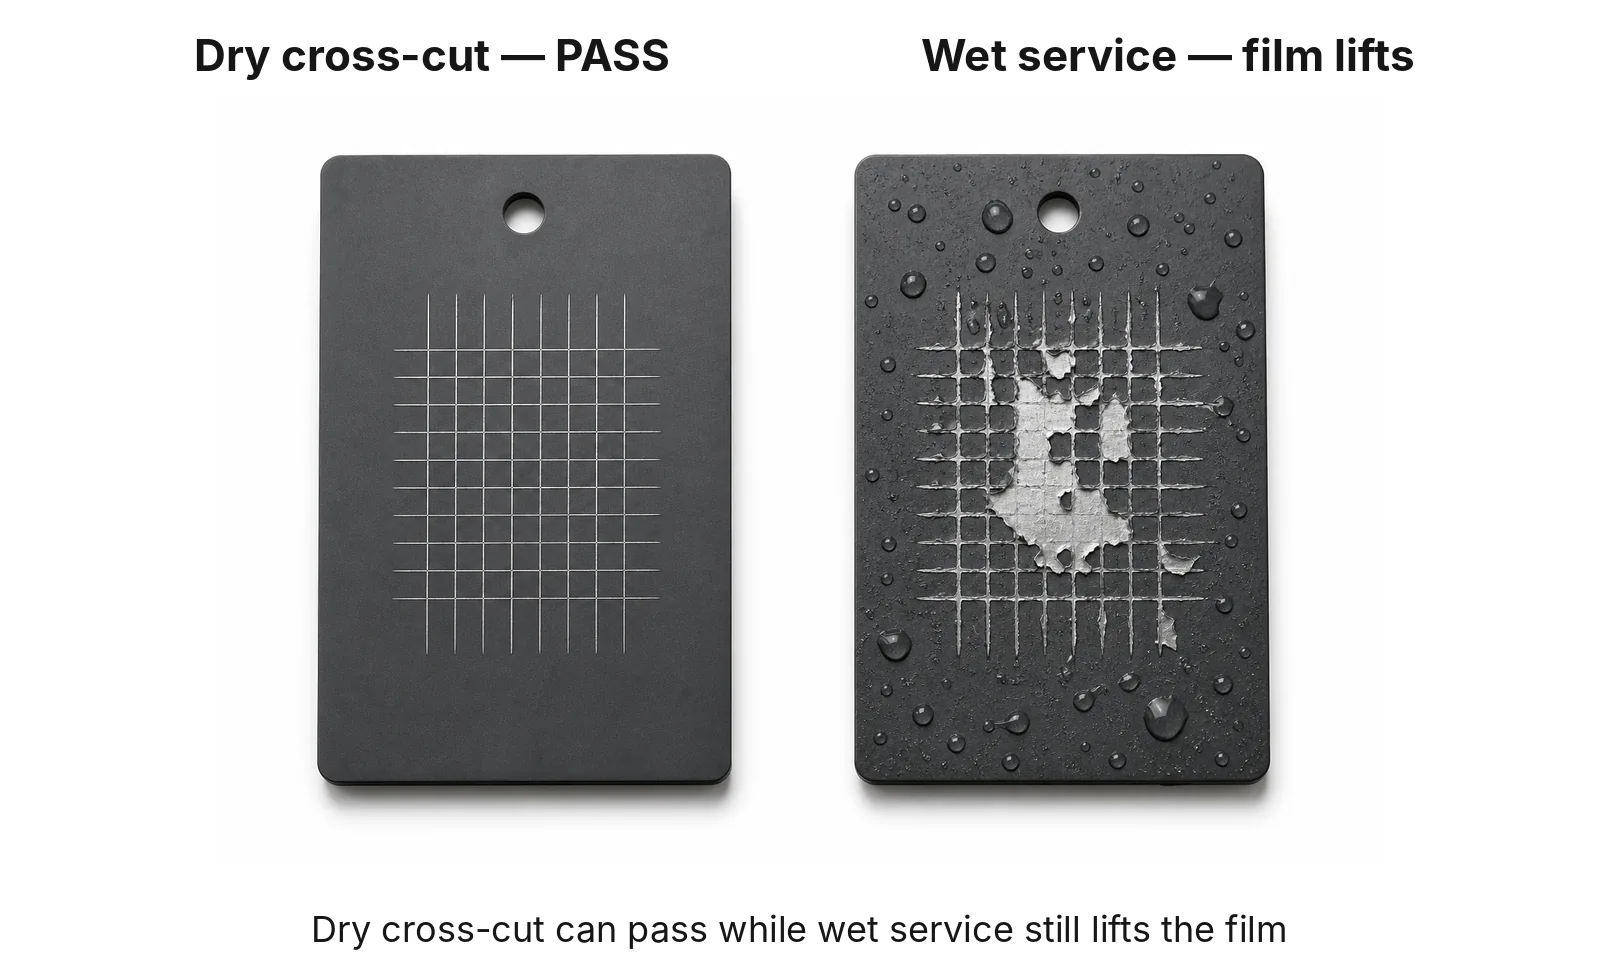
That is why wet adhesion matters for outdoor architectural luminaires—and for aluminum alloy housings on wall washers, linear lights, and floodlights.
Dry adhesion vs wet adhesion
Dry adhesion is what most quick lab screens measure: how well the film holds when the coating is dry. Wet adhesion is how that bond behaves after water, humidity, or salt exposure has stressed the coating–metal interface. Coatings practice has long treated the two as different questions (including Funke’s wet-adhesion discussion).
For outdoor corrosion protection, wet behavior usually matters more. A finish that survives a dry grid cut can still lose grip once water sits at the interface—the condition coastal, riverside, and bridge projects see for years.
Two methods you will see on North American projects
| Method | Standard | What it is used for | Limit |
|---|---|---|---|
| ASTM D3359 (tape / cross-cut; X-cut and cross-cut) | ASTM D3359 — Standard Test Methods for Rating Adhesion by Tape Test | Common dry screen on production and incoming checks. International counterpart often cited: ISO 2409 | A pass does not prove wet performance |
| ASTM D4541 (portable pull-off) | ASTM D4541 — Standard Test Method for Pull-Off Strength of Coatings Using Portable Adhesion Testers | Clearer read of bond strength at the interface. International counterpart often cited: ISO 4624 | Needs controlled setup; interpret against the project’s acceptance method |
Salt-fog exposure is commonly discussed with ASTM B117 — Standard Practice for Operating Salt Spray (Fog) Apparatus. Use B117 as exposure context for wet service risk, not as a published TPK hour rating.
Field tape pulls sometimes appear on site as a rough check. Treat them as informal only; engineering acceptance should follow the project’s written method.
Project language: corrosivity context, not a certification claim
ISO 12944 corrosivity categories (for example C3 / C4 / C5) give consultants a shared way to describe atmosphere and protection expectations. On many North American jobs, owners and coatings specs also point to SSPC/NACE (now AMPP) practice documents or project-specific finish requirements. That shared language is not a claim that a luminaire maker holds a particular coating-system certification.
For outdoor LED projects, ask whether the housing finish matches the moisture and salt reality of the elevation—and how wet-condition performance will be verified.
Where this lands on outdoor luminaires

Most outdoor architectural fixtures in this category use aluminum alloy housings—for example, extruded 6063 linear wall washers. Some floodlights use die-cast aluminum instead; do not mix the two when you name a specific product. On bridges, waterfront façades, and humid climates, the coating or anodized finish sees wet–dry cycles for the life of the install. Pretreatment, the finish as a system, and wet-condition verification belong in the same conversation as IP rating and optical performance.
IP rating covers water and dust ingress. Coating adhesion covers whether an organic finish stays bonded to the aluminum under wet service. Both matter; they are different tests.
What to ask in a submittal
Keep questions answerable without proprietary recipes:
Pretreatment + coating system
What pretreatment + coating / finish system approach is used on the aluminum alloy housing?
Dry screen in QC
Which dry screen is used in QC, if any—commonly ASTM D3359 (or ISO 2409 as an international counterpart)?
Wet-condition behavior
How is wet-condition behavior considered—salt-fog exposure context such as ASTM B117, humidity/condensation exposure, or project-specified wet checks? (Method language only—not invented hour claims.)
Site corrosivity language
How do acceptance criteria map to site corrosivity language (ISO 12944 categories and/or SSPC/NACE (AMPP) / owner specs) without over-claiming certifications?
Do not lock the bid to unverifiable details (exact grit, film thickness in μm, secret formulas) unless the contract requires them and the supplier can document them.
Soft note on factory capability
TPK Lighting builds outdoor linear and related architectural luminaires for façades, bridges, and infrastructure. In-house lab work includes salt-spray among other checks used in development and quality. Separately, IP67 validation on relevant products follows a multi-step waterproof sequence (aging, hot immersion, powered underwater run, then sort/rework). That sequence verifies ingress performance; it is not an adhesion test.
For photometrics, certificates, and technical files used in submittals, see Technical Resources and the related guides in the sidebar.
- ASTM D3359 — Standard Test Methods for Rating Adhesion by Tape Test (dry adhesion screens: X-cut / cross-cut)
- ASTM D4541 — Standard Test Method for Pull-Off Strength of Coatings Using Portable Adhesion Testers
- ASTM B117 — Standard Practice for Operating Salt Spray (Fog) Apparatus
- ISO 2409 / ISO 4624 — international cross-cut / pull-off counterparts
- ISO 12944 — corrosivity categories (C3/C4/C5) as shared project language
- SSPC/NACE (now AMPP) — practice documents often cited with owner specs on North American jobs